This case study demonstrates how the precise adaptation of a four-way shuttle racking system to the existing room height and warehouse footprint enabled intelligent, high-density modernisation of an ageing facility. In combination with WMS/WCS intelligent scheduling software, a goods-to-person automated solution was created that maximises available building space and greatly accelerates pallet storage and order fulfilment.
Location: Germany Industry: Aerospace Application: Automated storage & order picking of sensitive, high-value aerospace components Initial situation: Existing warehouse with restricted floor area and fixed ceiling height Solution: Custom-engineered four-way shuttle racking system integrated with intelligent shuttle robots and vertical lifts Objective: Boost storage density and throughput through warehouse intelligent retrofitting
The existing warehouse was constrained in both usable floor space and vertical clearance. Building extension or new-build construction was not financially viable. Valuable, sensitive aerospace parts required secure, traceable storage with fast access for production supply. The original manual forklift picking workflow was reliable yet inefficient: it consumed excessive aisle space, created long travel routes, carried higher product damage risks, and failed to fully exploit the available vertical height. Inventory tracking relied heavily on manual records, with limited real-time visibility.
The goal was to deploy an automated system that transforms the existing warehouse without structural modification or overcomplicated operation logic.
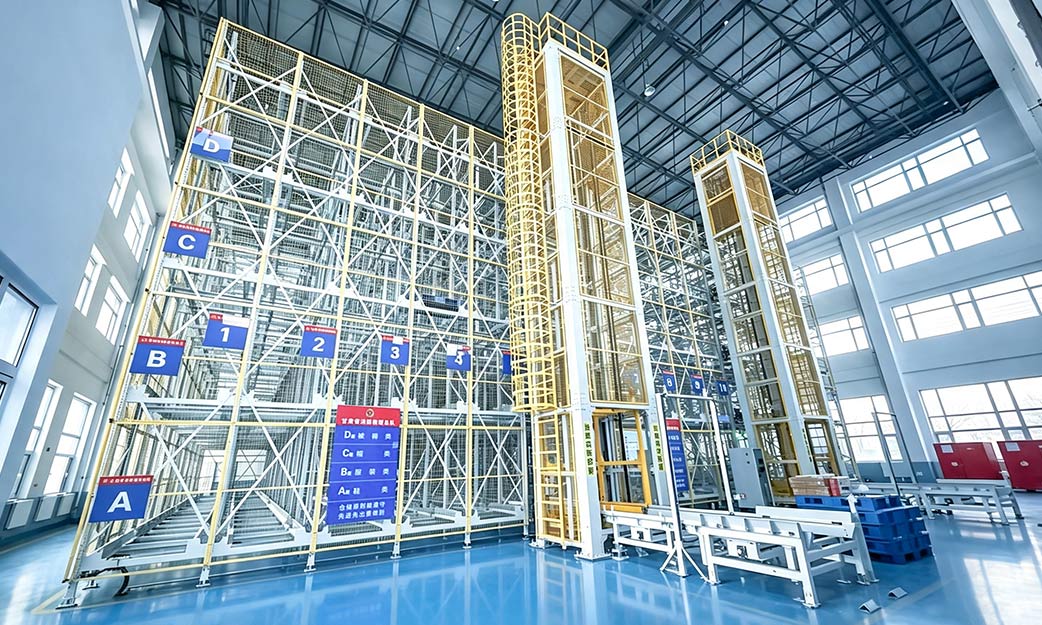
At the centre of the intelligent upgrade is a four-way shuttle racking system tailor-made for the warehouse’s actual dimensions. Rack elevation, lane depth, bay layout and transfer station positions are engineered to capture every inch of available vertical space. The racking infrastructure works with four-directional shuttle robots and vertical lifts. Controlled by integrated WMS and WCS software, shuttles travel freely forward, backward, left and right within the rack lanes, moving pallets between storage locations and transfer stations automatically.
The four-way shuttle racking forms the rigid, precision-guided storage backbone of the whole system. The shuttle robot acts as the flexible automated handling core. Pallets are automatically transported from deep storage lanes to the picking station, where operators complete value-added handling at an ergonomic workstation. No frequent forklift entry into dense storage zones is required. The system coordinates multiple shuttles dynamically to avoid congestion and sustain continuous inbound and outbound flow.
This modular concept can be replicated for many existing warehouse retrofits. The core principle is customising shuttle racking around the site’s physical constraints, then scaling robot quantities and software capacity according to growing throughput demands. It is an ideal automation route for businesses aiming to build high-density intelligent storage without investing in brand-new warehouse construction.
leave a message
Scan to Wechat :
Scan to WhatsApp :
Home
products
contact